Distinguish format from confirmed capability
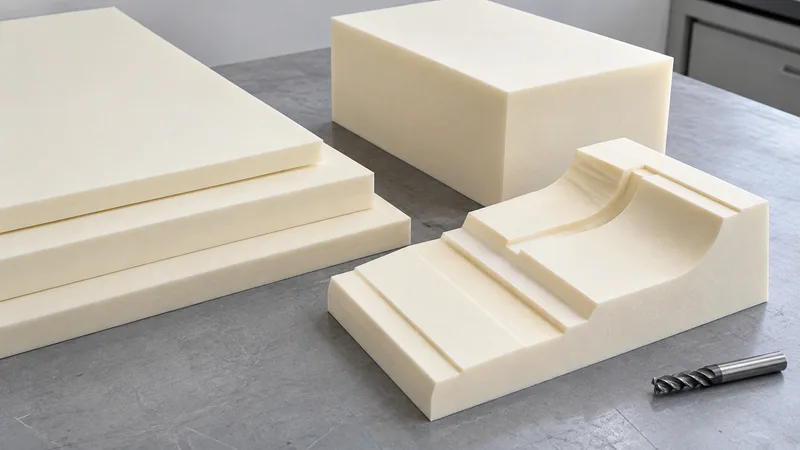
Rigid PU Foam sheets, blocks and CNC-cut cores are format routes for insulation layers, models and structural cores. The client knowledge base mentions mold-in-foam and CNC processing directions, but it does not confirm stock dimensions, equipment ownership, universal machining tolerances or a minimum feature size. Keep those fields pending confirmation for the proposed grade.
A sheet concept is useful when the component has predominantly planar sections. Ask which thickness, face condition and cut outline the project needs. A block concept can frame shaped or model work where stock preparation and orientation matter. Neither term proves that a particular size is kept in stock or can be delivered under an assumed lead time.
- Planar layer: locate the reference face and thickness requirement.
- Shaped stock: distinguish starting volume from the final envelope.
- Converted core: nominate pockets, steps and facing surfaces for inspection.
CNC-cut work expresses a drawing-controlled profile. The request should identify datums, machining faces, pockets, tool access and relevant tolerances. A molded concept introduces other tooling and forming questions. Do not treat molding and CNC as interchangeable processes merely because both can be discussed around the same outside shape.
Start at the Rigid PU Foam product hub with a controlled model and drawing. State which features are fixed and which may be revised. A format proposal becomes useful when it preserves the component purpose rather than presenting a generic claim that any shape is available.
Define stock, orientation and machining references
Show the final envelope and local thickness separately from the proposed starting stock. A block may be oriented to support a particular machining setup, and a sheet may require a reference face. Request confirmation of stock allowance and preparation instead of assuming the final dimensions define the starting material.
Mark the datum surfaces used by assembly and inspection. If one face meets a panel skin or a model fixture, identify it on the drawing. A machining reference that differs from the assembly datum can create a comparison problem unless the relationship is explicitly defined.
Record orientation in both the part drawing and any material evidence. Compressive-strength specimens and finished geometry need their own identified directions. Do not assume that a material result measured in an unspecified direction applies to a differently oriented core solely because the grade label is the same.
Keep critical tolerances distinct from informational dimensions. The knowledge base does not establish universal Rigid PU conversion capability. Ask the process owner to confirm which dimensions can be controlled, how they will be measured and what drawing revision represents the proposed manufacturing route.
| Decision field | Input or record | Review purpose |
|---|---|---|
| Sheet | Planar layer and section | Confirm face, thickness and outline |
| Block | Starting stock for shaped work | Confirm stock and orientation |
| CNC core | Datums, pockets and access | Confirm geometry and tolerance |
| Molded concept | Tooling and finishing proposal | Confirm actual route scope |
| Assembly | Facings, joints and hidden features | Plan inspection before joining |
Make features and edge treatments reviewable
Add sections through pockets, steps, tapered edges and local recesses. Identify the remaining thickness beneath each feature and the adjacent component it serves. A pocket that clears hardware and a recess that sets a facing position can have different priorities even when they look similar in a rendered model.
Identify feature access and the surfaces that must remain intact. A proposed toolpath or setup can require a change to geometry, but the reviewer must explain that change before the drawing is released. Do not promise a feature limit, cutter radius or surface finish that the client record has not confirmed.
Show how neighboring core pieces meet. A multi-piece insulation layer or assembled model needs part identification, edge alignment and a defined counterpart relationship. Record the thickness at each interface, the assembly reference surfaces and the inspection method. The project owner should define acceptance for the actual core construction.
If a facing or bond surface is involved, identify it separately from a trim surface. Ask what condition is required before joining and how it will be inspected. Actual adhesion, surface preparation and interface strength need evidence for the proposed construction; the format name alone cannot prove compatibility.
For a pocket that approaches a facing surface, show its depth from the nominated datum and the remaining local section on a separate detail. Ask the process reviewer to identify how that depth will be produced and inspected, including any access limitation. If another setup or a revised corner is proposed, place the change on the drawing for design review. The route proposal should resolve a specific feature rather than silently replace the geometry that the facing interface requires.
Compare CNC and molded proposals on the same drawing
A fair route comparison keeps function, critical sections and counterpart interfaces visible. Ask each proposed process to identify stock assumptions, forming or machining steps, finishing scope and inspection method. Record where the process requires a geometry adjustment rather than treating two similar looking samples as equivalent constructions.
For CNC work, identify machining references, access restrictions and the sequence needed to reach important features. For a molded concept, ask about tooling inputs, form features, revision handling and finishing. These are discussion questions, not statements that Green Foams operates every required process in-house.
The source ranges 30–200 kg/m³ and compressive strength 0.2–5 MPa remain pending confirmation. A process preference does not validate a grade. Use the density and strength guide to request the material record associated with each route.
Consult ASTM International and the ISO standards catalogue with the test owner for measurement terminology. Public method references do not establish a supplier machining tolerance or certify the resulting component.
Inspect before joining and after assembly
Plan dimensional inspection around the drawing datums and feature priorities. Check critical thicknesses, outline, pockets, edges and facing references before the core is concealed. Record the method and sample identity. This protects an important local section from being lost behind an otherwise acceptable external panel appearance.
Review how the core reaches the workstation or assembly fixture. Identify orientation, handling points and part separation for a multi-piece set. Damage or a version mix-up can obstruct a geometry review, so record the intended packing and identification inputs with the sample route.
Review pockets, alignment and access with the intended counterparts. Facing contact establishes fit only, not bond strength or thermal performance. Retain the approved grade/drawing and confirm stock, tooling and commercial terms separately.
Control format changes through procurement
Use the thermal and structural core selection guide when a format proposal affects the function. A change from a planar layer to a shaped core, or from a single piece to a set, can require another geometry and evidence review.
The cold-chain and construction brief preserves the route in quotation. State the final drawing, stock or process assumptions, material questions, counterpart references and inspection scope. Ask proposals to identify their differences from that baseline.
Send a feature-based conversion request
Ask for a route response against individual features, not an unqualified claim that CNC or molding can make the part. A pocket is defined by its depth from a datum and remaining section; a bond face is defined by its interface role. The same outside envelope can conceal a different local construction.
| Drawing feature / purpose | Required delivered condition | Supplier route and inspection response |
|---|---|---|
| [pocket detail / hardware clearance] | [datum, depth and remaining section from drawing] | [proposed access, measurement and exceptions] |
| [facing-contact surface] | [drawing reference and required condition] | [pre-joining inspection; excluded interface work] |
| [matching edge in a piece set] | [neighbor identity and alignment reference] | [identification and paired-fit check] |
| [route alternative] | [features that must remain unchanged] | [CNC / molded proposal; changed features and tooling scope] |
For quotation, distinguish starting stock, converted core, tooling and facing attachment as separate deliverables. Leave unconfirmed stock sizes, feature limits, tolerances and commercial terms open. The first article should close the nominated feature questions; material compression and thermal evidence remain separate.
- Check accessible sections before the facing conceals them.
- Escalate a proposed corner, datum or remaining-section change to the drawing owner.
- Retain the paired-edge record when one core becomes a multi-piece set.